Sealless Pumps for a Safer and Greener World

Choosing the right concrete mixer can influence project speed, batch consistency, labor costs, and maintenance planning. For global buyers, the 2026 search for a Js1500 Concrete Mixer requires more than comparing catalog prices. A serious evaluation should examine mixing performance, steel quality, motor configuration, discharge design, spare parts support, and delivery conditions.
The JS1500 model is commonly associated with a twin-shaft mixer and a nominal mixing capacity of about 1.5 cubic meters per batch. Its performance depends on concrete formulation, aggregate size, moisture content, and operating discipline. A well-built unit should produce a uniform mixture while maintaining stable operation during demanding construction cycles. However, advertised capacity does not always equal practical output. Site conditions matter.
Details matter most.
Experienced buyers should request technical drawings, motor specifications, liner materials, warranty terms, and inspection records. Supplier experience with international shipping can also reduce avoidable delays. Electrical standards, safety requirements, foundation dimensions, and local service availability deserve careful review before payment. These checks support a more reliable purchasing decision and help reduce future downtime.
This guide compares important features of the 2026 Best JS1500 Concrete Mixer options for global applications. It also considers supplier credibility, customization, installation guidance, and long-term operating value. Some recommendations may appear obvious, yet they are often overlooked during rushed purchasing. The best choice is not automatically the cheapest machine. It is the mixer that matches your production needs, site limitations, budget, and support expectations. That judgment requires evidence, not promises.
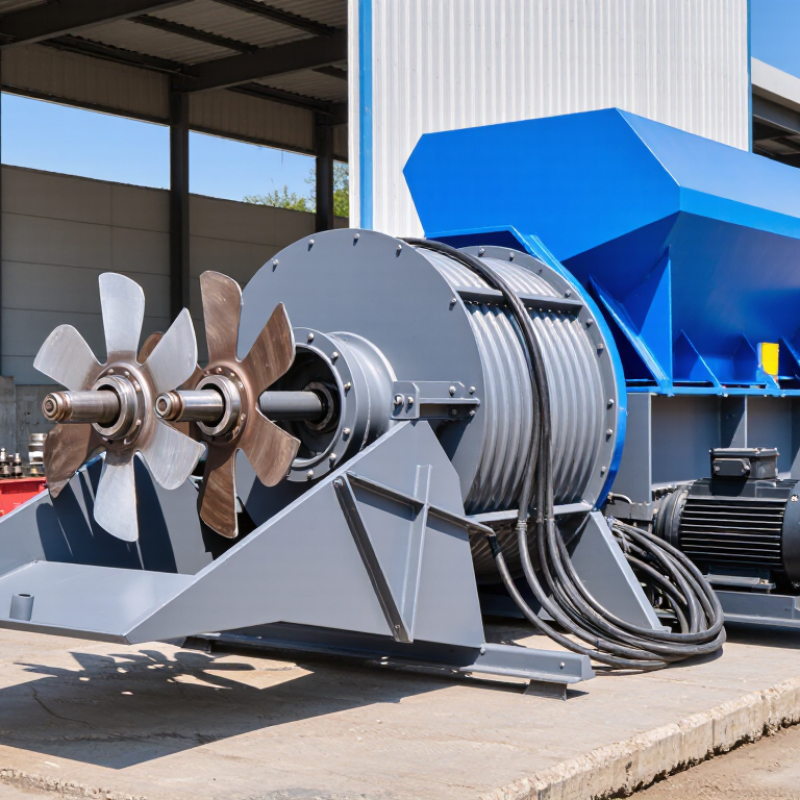
A JS1500 concrete mixer is built for a nominal 1.5 m³ batch. Its twin-shaft design uses two horizontal shafts rotating through the mixing chamber. Paddles lift, split, and fold the materials repeatedly. This action helps distribute cement paste around coarse aggregate and sand. The result can be a more consistent mix than basic single-shaft equipment.
Real output depends on loading habits and material conditions. Do not treat 1.5 m³ as an unrestricted daily target. Moisture in sand changes the water balance, sometimes more than operators expect. Accurate weighing is essential. Calibrate cement, aggregate, and water systems regularly. Keep the charging sequence consistent, and avoid overfilling the chamber. A practical batch often needs enough mixing time for uniform color and texture, not merely a fixed timer.
Small details matter. Check paddle clearance before production. Inspect shaft seals, liners, and discharge-gate movement during routine maintenance. Hardened concrete around the gate can create uneven discharge and unnecessary strain. In field operation, I have found that operators sometimes increase water to solve poor workability. That shortcut may weaken the designed mix. A better response is checking aggregate moisture, dosing accuracy, and mixing time. Even experienced teams can miss one reading during a busy shift. Record batch weights, moisture results, and discharge observations for reliable quality control.
The JS1500 concrete mixer uses a 1.5 m³ nominal batch size. Its theoretical output can reach 75 m³/h under tightly controlled conditions. The calculation is simple: 50 batches per hour multiplied by 1.5 m³. Each complete cycle must finish in about 72 seconds. That cycle includes aggregate loading, water and cement dosing, mixing, and discharge.
Real projects rarely match the laboratory figure. Material moisture changes throughout the day. Sticky aggregate may slow loading and reduce mixing efficiency. A well-calibrated weighing system helps maintain batch accuracy. Operators should also inspect mixing blades, discharge gates, and hydraulic parts regularly. Small delays matter. A three-minute stoppage can remove several cubic meters from the hourly schedule.
From field practice, consistent feeding usually matters more than aggressive machine settings. The loader should supply aggregate smoothly, without striking the hopper. Mixing time must suit the concrete grade, slump, and admixture dosage. Overloading can create uneven material and increase wear. Underfeeding wastes available capacity. The 75 m³/h figure is therefore a planning reference, not a guaranteed result. Site layout, truck availability, power stability, and operator skill can lower practical production. That gap deserves honest calculation before purchase.
2026 Best JS1500 Concrete Mixer for Global Buyers
The JS1500 mixer is designed for demanding production where cycle speed and batch uniformity matter. In practical use, a 30–60-second mixing cycle can work well, but timing depends on material conditions. Dry aggregates often need longer blending. Excess water can create paste pockets and uneven slump. Operators should check moisture, aggregate grading, and loading order before judging mixer performance.
Uniformity control requires more than a fast motor. Twin-shaft movement should distribute cement, sand, stone, and water across the full mixing zone. Inspect blade clearance regularly, especially after handling abrasive aggregates. A small clearance change can create dead areas. I have seen acceptable batches become inconsistent after several weeks of poor adjustment. That result is easy to overlook.
Tips: Start with a 45-second cycle, then test the batch visually and through slump checks. Record water content and discharge time for each load. Keep loading intervals consistent. Do not shorten the cycle only to increase output. A faster batch may reduce quality. Also, verify control settings with local technicians, because material behavior changes between regions. Even experienced crews can misread uniformity under changing weather.
| Data Dimension | Typical JS1500 Reference Data | Practical Interpretation for Global Buyers |
|---|---|---|
| Mixer type | Horizontal twin-shaft forced-action concrete mixer | Suitable for ready-mix concrete, precast production, block making and infrastructure projects. |
| Nominal discharge capacity | 1.5 m³ per batch | The batch size is measured as compacted concrete discharge volume; actual output depends on the mix and operating cycle. |
| Typical production rate | Approximately 60–90 m³/h under continuous plant operation | Theoretical capacity is based on cycle time; loading, discharge, material dosing and site logistics reduce real output. |
| Recommended total cycle | 30–60 seconds per batch, excluding long material-loading delays | Shorter cycles are achievable with efficient feeding, correct moisture control and a properly configured discharge system. |
| Typical mixing stage | 15–30 seconds after all main ingredients enter the mixing chamber | The optimum time varies with slump, aggregate grading, cement content, admixtures and required uniformity. |
| Mixing uniformity control | Controlled through calibrated batching, consistent feed sequence, moisture correction and timed mixing | Uniformity should be verified by sampling fresh concrete at different discharge points and testing according to the applicable local standard. |
| Aggregate size compatibility | Commonly configured for aggregate sizes up to approximately 80 mm | The allowable size depends on shaft, paddle, liner and discharge-gate configuration; confirm before ordering. |
| Drive arrangement | Two electric drive motors are commonly used for twin-shaft operation | Motor voltage, frequency, enclosure rating and installed power must match the destination site's electrical supply. |
| Typical installed power range | Approximately 55–75 kW, depending on configuration and duty requirement | Higher-moisture mixes, heavy aggregates and frequent high-load operation may require a larger drive configuration. |
| Discharge gate | Bottom discharge gate, commonly hydraulic or pneumatic | Select the actuator and outlet arrangement according to plant layout, cleaning access and required discharge speed. |
| Wear protection | Replaceable wear liners and abrasion-resistant mixing paddles | Liner thickness and material should be selected according to aggregate abrasiveness and expected operating hours. |
| Moisture-management requirement | Moisture measurement or routine correction is recommended for sand and aggregates | Correcting aggregate moisture helps maintain water-cement ratio, slump consistency and batch-to-batch uniformity. |
| Quality-control checkpoints | Batch weighing, water metering, mixing-time control, slump checks and periodic strength tests | A mixer alone does not guarantee concrete quality; the complete batching and testing process determines results. |
| Recommended cleaning interval | Clean after each production shift and remove buildup before hardened concrete forms | Regular cleaning protects mixing efficiency, reduces wear and helps maintain the designed working volume. |
| Best-fit applications | Medium-to-high-volume concrete production requiring repeatable batch quality | A practical choice for commercial batching plants, precast yards, road projects and large construction sites. |
A JS1500 mixer should be judged by compliance, not only batch volume. Industry reports from the Global Cement and Concrete Association estimate annual concrete production at about 14 billion cubic metres worldwide. That scale makes reliable electrical integration essential. A three-phase motor usually supports stable torque under heavy mixing loads. Buyers must still confirm voltage, phase sequence, motor insulation, and local control-panel requirements. Both 50 Hz and 60 Hz options matter. A frequency mismatch can reduce efficiency or damage components.
A three-phase motor usually supports stable torque under heavy mixing loads. Buyers must still confirm voltage, phase sequence, motor insulation, and local control-panel requirements. Both 50 Hz and 60 Hz options matter.
CE marking supports access to applicable European markets, but it is not a universal quality certificate. Suppliers should provide a Declaration of Conformity, risk assessment, technical files, and safety instructions. ISO 9001 is different. ISO’s 2022 Survey recorded more than 1.2 million ISO 9001 certificates globally, showing how widely quality systems are used. Yet certification alone cannot prove a mixer’s durability. Ask for factory test records, welding procedures, gearbox data, and spare-parts response times. Details matter.
A nominal 1.5 cubic metre batch may vary with moisture, aggregate size, and loading practice. Experienced buyers should request a witnessed trial using local materials. This step is often skipped, and that is a weakness.
Confirm cycle time, current draw, emergency stops, guarding, and cleaning access before shipment.
Some specifications look complete but hide important assumptions.
A careful inspection remains more reliable than attractive paperwork.
For global buyers, a JS1500 lifecycle review should begin with site records, not brochure capacity. In field-service inspections, liner plates, mixing blades, shaft seals, and discharge-gate components often decide downtime. Abrasive aggregates can thin a liner faster than expected. Moisture and poor cleaning can damage seals within weeks. Keep a monthly wear log. Record thickness, operating hours, aggregate type, and replacement cost.
Energy use deserves the same discipline. A practical test measures kWh per cubic meter across several batches, including startup and idle time. A long mixing cycle may look efficient while the mixer waits between loads. Variable production matters. For five-year planning, multiply measured energy by local electricity rates and annual output. Add labor, grease, inspections, spare parts, freight, and planned downtime. Small leaks become expensive.
An illustrative five-year TCO model should include purchase, installation, wear parts, power, maintenance, and lost production. Buyers should request service records and a parts list before comparing quotations. I would not trust a low purchase price without a realistic liner replacement schedule. My estimate may be imperfect because aggregate hardness, climate, and operator habits vary sharply. Use low, normal, and severe abrasion scenarios. Recheck the model after the first 500 operating hours. That early correction can expose assumptions that looked reasonable on paper.


